Languages
Brand-Compatible Screw and Barrel Replacement: Ordering from OEM Drawings
-
Brand-Compatible Screw and Barrel Replacement: Ordering from OEM Drawings
A KraussMaffei KMD, Battenfeld-Cincinnati twinEX or Theysohn screw and barrel can be replaced without the original sample — from drawings, measurements or reverse engineering. Here is what to send, what to measure, and how to make sure the replacement actually matches the original metallurgy and bore.
-
BRAND-COMPATIBLE SCREW BARREL · REPLACEMENT SCREW BARREL · KRAUSSMAFFEI KMD · COUNTER-ROTATING TWIN SCREW
-
1. What a Brand-Compatible Replacement Actually Is
A brand-compatible screw and barrel is a part made to the original machine’s specification, so it drops straight in where the OEM part went — same bore, same flight profile, same spline, same material. It is a reverse-engineered or drawing-driven replacement, built by a specialist screw and barrel manufacturer rather than ordered back through the machine maker’s spares channel.
Two situations make it the sensible route. The machine is out of production and the OEM no longer stocks the part, or the OEM price and lead time are unattractive against a like-for-like replacement. The drop-in constraint only fixes the dimensions; the material is a decision you are free to improve — for example moving a worn nitrided barrel to a bimetallic one.
-
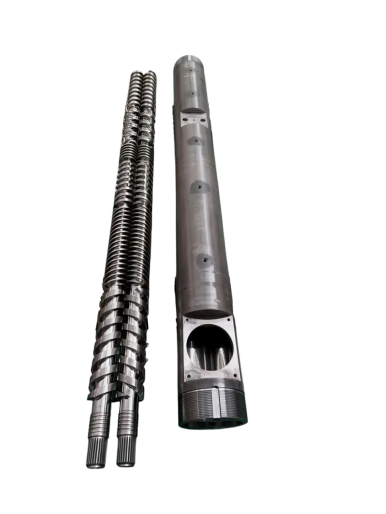
A KraussMaffei KMD counter-rotating parallel twin screw and barrel. A brand-compatible replacement means matching the original bore, spline, flight profile and metallurgy — not just the model number.
-
2. The Brands and Series We Cover
Brand / series Machine type Typical screw range Replacement coverage KraussMaffei KMD Counter-rotating parallel twin KMD 40 – KMD 130 Screw, barrel and matched set Battenfeld-Cincinnati twinEX Counter-rotating parallel twin twinEX 72 – twinEX 135 Screw, barrel and matched set Theysohn XTS Counter-rotating parallel twin XTS series Screw, barrel and matched set Bausano MD Counter-rotating parallel twin MD 66 – MD 130 Screw, barrel and matched set Kabra Counter-rotating parallel twin Series per model Screw, barrel and matched set Luigi Bandera 2B HTS Counter-rotating parallel twin 2B HTS series Screw, barrel and matched set Mikrosan MCV Counter-rotating parallel twin MCV series Screw, barrel and matched set Weber DS Counter-rotating parallel twin DS series Screw, barrel and matched set Screw and barrel are supplied and measured as a matched pair, because the meshing clearance of a twin screw is what sets both output and wear life.
-
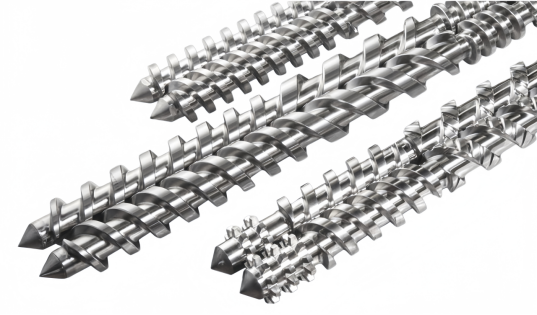
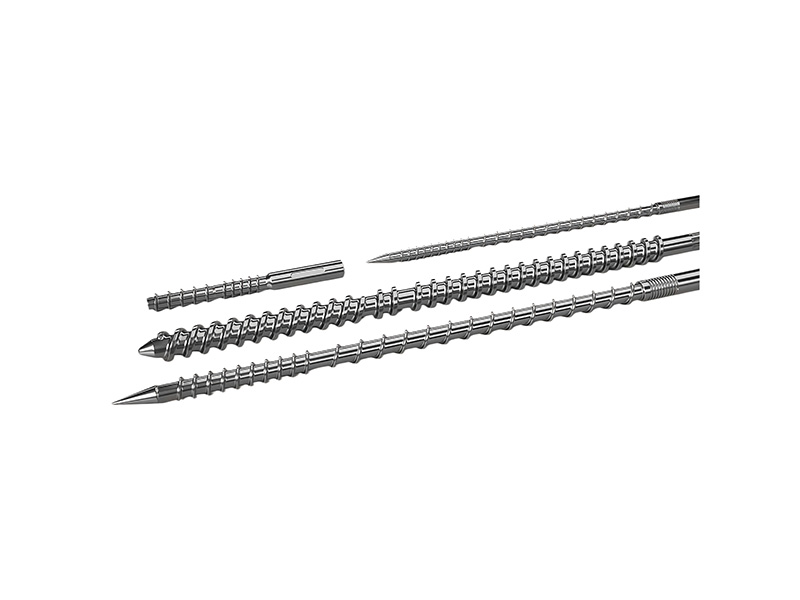
Brand-compatible extruder screws for different machine series. Coverage spans the counter-rotating parallel twin machines used in pipe and profile lines.
-
3. What You Need to Order
Input What it gives When to use it Original drawing / part number Every dimension, tolerance, material and treatment Always the first choice — fastest and most exact Worn sample returned Physical part to measure and reverse-engineer When no drawing survives Field measurements The key diameters and lengths read off the machine When neither drawing nor sample is available KEY INSIGHT — Send the worn part back. A used screw is the single most valuable piece of information in a replacement job — the wear pattern on it tells the supplier exactly what failed and which geometry to correct.
-
4. Reverse Engineering from a Worn Part
When the drawing is gone, the worn part becomes the master. Reverse engineering measures the surviving geometry and reconstructs the original by adding back the material that wear has removed.
Dimensional survey — outside diameter, root diameter, pitch, flight width, spline, overall length, measured along the part with the wear zones noted.
Wear compensation — the flight and bore dimensions are corrected back to nominal, using the unworn regions as the reference.
Metallurgy identification — the base steel and surface treatment are identified so the replacement matches the original hardness and case depth.
Pair matching — the screw and barrel are treated as one assembly, so the reconstructed clearance is what the pair originally ran at.
-
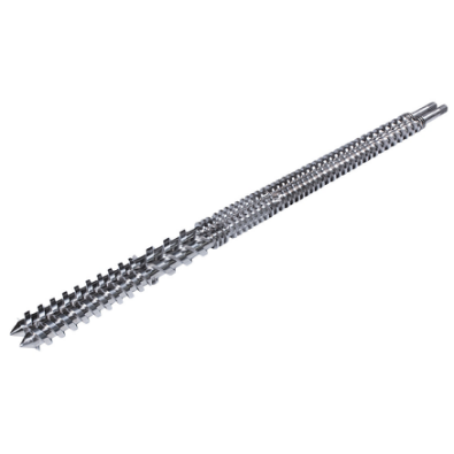
A complete counter-rotating parallel twin screw assembly. The reconstructed part is produced to a drawing you approve before metal is cut.
-
5. Measuring a Worn Screw and Barrel
Dimension Where to measure Why it matters Screw outside diameter Flight tips, several axial positions Sets the flight-to-bore clearance Screw root / core diameter Bottom of the channel Sets the channel depth and the compression ratio Pitch / lead Axial distance per full turn Sets the conveying and mixing character Flight width and flank angle Flight cross-section Affects shear, mixing and wear resistance Spline specification Drive end of the shaft Must match the gearbox and the coupling Barrel bore diameter Inside the barrel, several positions Sets the operating clearance Overall screw and barrel length End to end Fixes the L/D and the barrel sectioning Wear pattern and depth Highest-wear zones Tells the builder where to harden the replacement Measure with a micrometer and a caliper, not a tape. The clearance between a twin screw pair is a fraction of a millimetre.
-
6. Drawing vs Sample vs Measurement
Criterion Drawing Worn sample Field measurement Accuracy Highest — nominal dimensions and tolerances High — reconstructed from the part Moderate — limited to measurable surfaces Speed to quote Fastest Medium — survey first Slowest — data may need clarification Metallurgy Specified on the drawing Identified from the part Must be inferred or specified separately Best when Original documentation survives Part is worn but complete Nothing else is available -
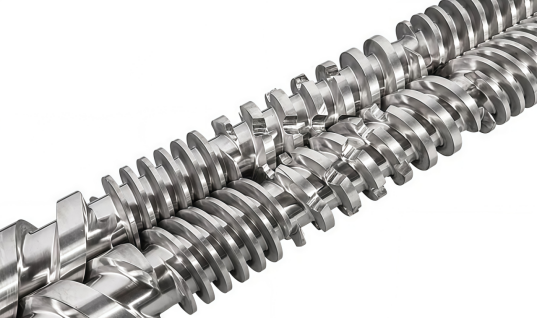
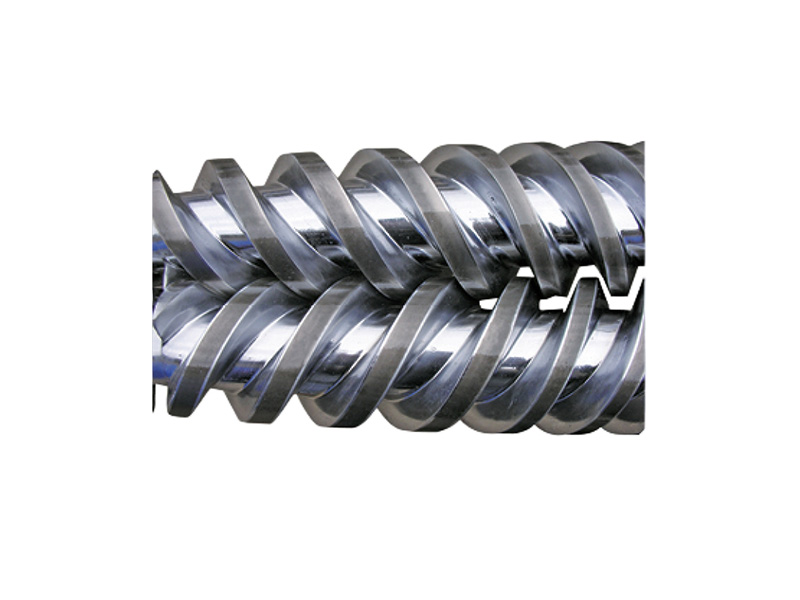
Close-up of intermeshing twin screw mixing elements. Flight clearance and disc geometry control leakage flow, shear intensity and element life under abrasive fillers.
-
7. Material and Treatment Matching
Original treatment Replacement equivalent When to keep / upgrade Nitrided barrel Deep gas-nitrided bore, HV 950–1,000 Keep for unfilled PVC; upgrade to bimetallic for abrasive feed Bimetallic barrel Centrifugal-cast nickel/cobalt/tungsten-carbide liner, HRC 58–65 Keep for high-wear duty; match the original alloy family Nitrided screw Nitrided flight, HV 950–1,000 Keep for unfilled; upgrade to hardfaced flight for filled compounds Hardfaced screw Plasma / HVOF bimetallic flight, HRC 58–64 Keep or upgrade the alloy grade for longer life Through-hardened screw Through-hardened alloy steel, HRC 58–62 Keep where uniform section hardness is needed A bimetallic liner in place of a nitrided one costs more up front but runs 3–6× longer on abrasive feed.
-
8. Cost and Lead Time
Replacement cost is set by diameter and L/D, metallurgy, whether it is a matched pair, and how much reverse engineering is needed. Lead time is normally measured in weeks once the drawing is confirmed — shorter than a discontinued OEM part.
-
9. RFQ Checklist
Item Notes Machine OEM, model and serial Fixes the machine the part must fit Screw diameter and L/D The two numbers that anchor every other dimension Drawing, worn sample, or measurements Whichever is available — the drawing is preferred Material being processed Filler and fibre loading decide the alloy and treatment Current failure / wear mode Tells the workshop where to harden the replacement Metallurgy requirement Match the original or upgrade — state the preference Quantity and urgency Sets the batch and the schedule -
10. Frequently Asked Questions
Can you replace a discontinued extruder?
Yes — with a drawing or the worn part, the original geometry is reconstructed even when the OEM no longer stocks the component.What if I don’t have the original drawing?
Send the worn part or a set of field measurements. The reverse engineering route reconstructs the geometry from what survives.How accurate is reverse engineering?
On a worn but complete part, to within a few hundredths of a millimetre.Do you need the worn parts back?
Strongly recommended. The wear pattern is the clearest signal of what to correct and where to harden.Will the replacement match the original metallurgy?
Yes — or upgraded deliberately. A nitrided barrel can be replaced with a bimetallic barrel for longer life on abrasive feed. -
Need a Brand-Compatible Screw and Barrel Quoted?
Send the machine OEM, model and serial, the screw diameter and L/D, and whatever survives — drawing, worn part or measurements — together with the material you run. PIPLL is an extruder screw and barrel manufacturer working in Φ20–500 mm and up to 12 m.
Eric Dong | Co-founder | Email: eric@pipll.com | WhatsApp: +86-15267878906 | Website: www.pipll.com